Key Considerations for Rotationally Molded Parts in Kansas
Key Takeaways
- Successful rotomolded parts are designed around the manufacturing process, material behavior, and real service conditions.
- Consistent wall sections, rounded transitions, proper venting, and targeted reinforcement help improve quality and durability.
- Kansas product teams should account for outdoor exposure, demanding work environments, transport, and seasonal temperature changes when defining performance requirements.
- Rotational molding is often a strong fit for large, hollow parts and lower-to-mid production volumes, while cycle time must remain part of the plan.
- Testing, repairability, material efficiency, and realistic end-of-life planning should be addressed before final tooling is approved.
From agricultural equipment and utility containers to protective housings and recreational products, Kansas manufacturers need plastic components that can handle real work. View more details here about rotational molding capabilities before committing a concept to a final mold for teams evaluating custom hollow parts. Better rotationally molded parts begin long before production. A CAD model may look clean and functional, yet still create difficulties with material flow, cooling, demolding, wall thickness, or long-term performance. The best results come from treating design, tooling, material selection, and testing as connected decisions.
Why Early Design Decisions Matter
Early design reviews give engineers a chance to identify risks while changes are still inexpensive. A broad flat panel may need reinforcement. A deep corner may require a smoother transition. A molded-in insert may need a different placement to support reliable manufacturing and assembly. Addressing these details before tooling begins can reduce rework and help a project move from prototype to production with fewer surprises. For Kansas-based projects, the part’s environment should guide the conversation. A tank used for fertilizer or cleaning chemicals has different requirements than a vehicle enclosure, livestock product, medical housing, or outdoor storage component. Define what the part must do before choosing the resin, shape, finish, or wall thickness.
How Rotational Molding Shapes Part Design
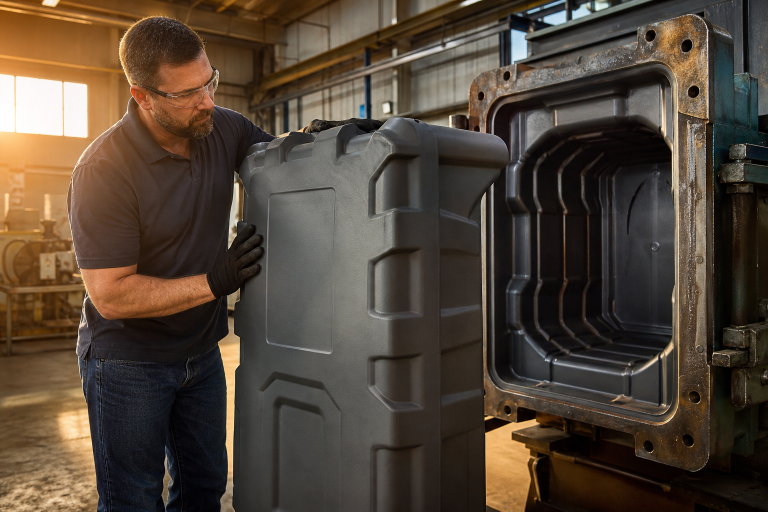
Rotational molding forms a hollow plastic part by placing a measured amount of resin, often in powder form, inside a closed mold. The mold rotates on two axes while heating, allowing the material to coat the interior surface, fuse, cool, and solidify before removal. Designers can review the rotational molding design guide for a deeper explanation of the process and its design considerations. This process does not force molten plastic into a mold cavity under high pressure. Instead, heat, time, rotation, mold geometry, and cooling behavior all influence the finished part. That is why a feature that works well in injection molding may need to be redesigned for rotational molding.
Start With the Part’s Main Job
Write a clear performance brief before refining the part geometry. Include the expected load, impact exposure, mounting method, cleaning requirements, storage conditions, service life, and safety expectations. Consider whether the part will hold a liquid, carry equipment, protect sensitive contents, float, stack, or be moved frequently by workers. For example, a large equipment cover may prioritize impact resistance, UV stability, secure attachment points, and stiffness across wide panels. A fluid-handling component may place more emphasis on chemical compatibility, leak resistance, fitting locations, and pressure testing. The part’s job should determine the design priorities.
Plan Wall Thickness and Transitions Carefully
Uniform wall thickness is generally easier to manufacture and can support more predictable cooling and performance. Abrupt changes in thickness can create uneven sections that complicate the molding cycle. Adding material throughout an entire part is not always the most efficient way to increase strength, as it can increase weight, resin use, and cycle time.
- Keep wall sections as consistent as practical.
- Use gradual transitions between thick and thin areas.
- Review corners, cutouts, and attachment zones for potential thin spots.
- Confirm the target wall thickness through prototype measurements and testing.
Use Radii, Ribs, and Kiss-Offs Wisely
Rounded corners help avoid abrupt stress concentrations and support smoother material distribution. Large flat surfaces can flex under load, especially on oversized housings, lids, and containers. Instead of making every wall thicker, designers can use carefully placed ribs, contours, or kiss-offs to add stiffness where it is needed. A kiss-off connects opposing interior walls at selected locations, providing structural support within a hollow space. Ribs and molded contours can also improve rigidity, but they should be reviewed with the tooling team to confirm they can be filled, cooled, released, and perform as intended.
Choose Materials for Actual Service Conditions
Material selection should be based on exposure, not simply initial cost or preferred color. Polyethylene grades are commonly used in rotational molding, but the appropriate formulation depends on the application. Review the following questions with the material supplier and manufacturer:
- Will outdoor use require UV-stabilized material?
- Will the part contact chemicals, fuels, cleaners, food, or potable water?
- Does the part need to retain impact resistance in colder conditions?
- Will repeated loading, vibration, or abrasion affect the part?
- Are there regulatory, sanitation, or traceability requirements?
Match Tooling to Volume and Detail
Tooling should fit the product’s size, surface expectations, tolerance needs, expected annual demand, and likelihood of future design changes. Simpler tooling can be useful for prototypes, larger industrial shapes, and early validation. More refined tooling may be appropriate when appearance, repeatability, texture, or detailed features are essential. Production planning also matters. Rotational molding can be a practical choice for custom, replacement, pilot, and specialized product programs, but its heating and cooling cycles should be considered when setting output expectations. Evaluate total project cost, not just the mold price.
Compare the Process to Other Options
- Rotational molding: Often suited to large, hollow, seamless parts with integrated features and flexible tooling needs.
- Injection molding: Often suited to detailed, repeatable parts where higher-volume production can justify more substantial tooling investment.
- Blow molding: Often used for hollow products such as bottles, containers, and other shapes that fit its process capabilities.
No process is automatically best. The right choice depends on part geometry, functional requirements, cosmetic expectations, production quantity, tooling budget, and delivery needs.
Build Sustainability and Testing Into the Plan
Sustainability should be evaluated through practical design choices. Reduce unnecessary material, consider recycled-content options only after validating performance, and design for a service life that fits the application. Where practical, make components easier to repair, replace, or separate from non-plastic hardware. Analysis can identify likely stress areas, but physical testing confirms how the actual part performs. A sound validation plan may include wall-thickness checks, dimensional inspection, load testing, impact testing, leak or pressure testing, chemical exposure testing, and trial assembly with mating components.
Common Mistakes to Avoid
- Applying injection-molding rules without considering rotational molding behavior.
- Using sharp corners and unsupported broad panels.
- Ignoring venting, cooling, draft, and demolding needs.
- Selecting a resin before defining the service environment.
- Waiting until final tooling to involve manufacturing and tooling specialists.
- Assuming recycled material will deliver identical results in every application.
Questions Designers Often Ask
What products work well with rotational molding?
Tanks, enclosures, containers, flotation products, protective housings, equipment covers, and recreational components can be good candidates when a large hollow form and durable one-piece construction are useful.
How can designers reduce warping?
Use balanced geometry, smooth transitions, practical wall planning, controlled cooling, and prototype testing. Warping can have multiple causes, so the part, mold, material, and process should be reviewed together.
When should the tooling team join the project?
Bring the tooling team in during early concept reviews. Their input can help identify features that may be difficult to mold, vent, cool, release, inspect, or assemble.
Final Design Review Checklist
- Define the part’s purpose, load cases, environment, and expected service life.
- Review wall thickness, corners, flat panels, reinforcements, and transitions.
- Confirm material compatibility with UV exposure, impact, chemicals, and temperature conditions.
- Match tooling and production planning to the product’s volume and quality requirements.
- Establish prototype, measurement, and performance-testing steps before full production.
For Kansas product teams, successful rotational molding design is a disciplined balance of function, manufacturability, and field performance. When those decisions are made early, the resulting part is more likely to be efficient to produce, dependable in service, and ready for the conditions it was built to face.
Conclusion
Successful rotational molding projects begin with a clear understanding of what the finished part must do and the conditions it will face. Kansas manufacturers should consider geometry, wall thickness, material compatibility, reinforcement, tooling, production volume, and service conditions as connected decisions rather than separate steps. Early collaboration between product designers, engineers, tooling specialists, material suppliers, and manufacturers can help identify potential issues with material distribution, cooling, venting, demolding, assembly, and long-term performance before final tooling is approved. Prototype parts and physical testing can also provide useful information about fit, strength, dimensions, impact resistance, chemical exposure, or other application-specific requirements. Production planning should account for cycle time, tooling costs, material efficiency, repairability, and realistic future demand. By reviewing these factors before production begins, Kansas product teams can reduce avoidable redesign work and make more informed manufacturing decisions. A disciplined approach to design and validation can help create rotationally molded parts that are practical to produce, consistent in quality, and suited to the real environments in which they will be used.